NEW & BLOG
Build a highly cohesive team of thermal management, special welding and
precision manufacturing
The Overlooked Heart of Friction Stir Welding: Inside a 1,000+ Tool Design Library
Sep. 29, 2026
Friction stir welding has a paradox at its center. The physics — a rotating tool that plasticizes and forges metal without melting it — is elegant, widely published, and more than three decades old. The equipment is now sold by several vendors worldwide. Yet weld outcomes between two suppliers running identical machines on identical alloys can differ by a wide margin. The variable that explains most of the gap is the smallest, least glamorous part of the system: the stirring tool itself.
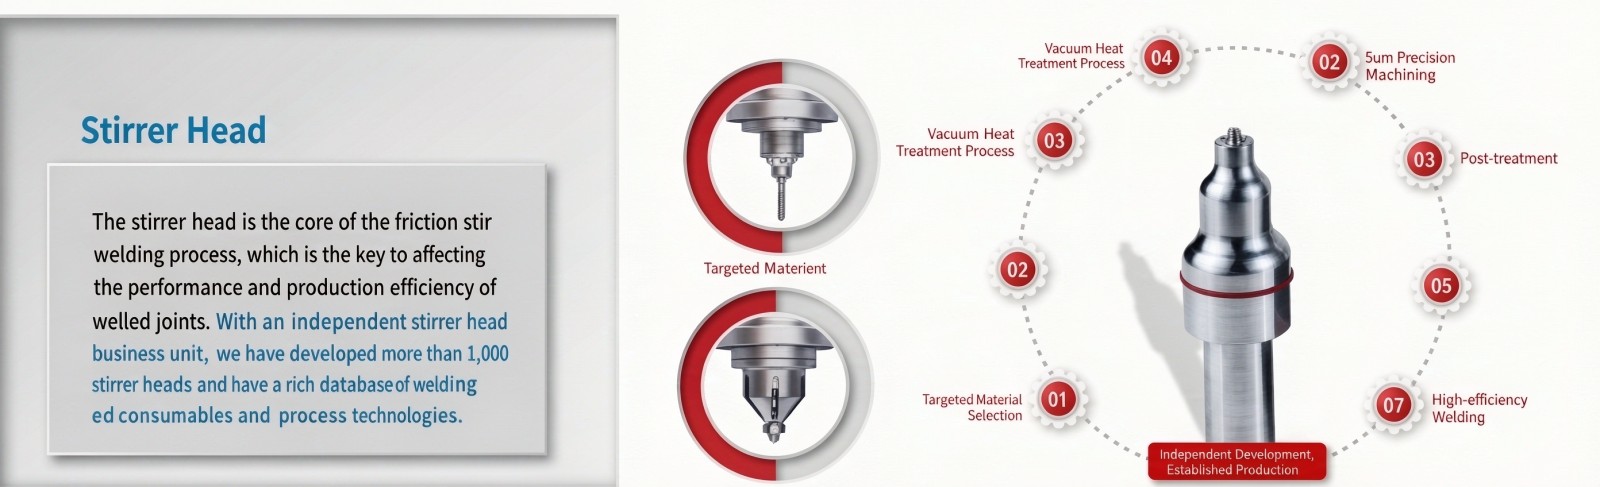
What the tool actually does. The tool's shoulder forges the softened material and controls flash; the pin stirs the joint, determines material flow, and sets the bonded volume. Tool geometry governs heat generation, travel speed tolerance, defect sensitivity, and achievable joint strength. Tool material governs wear life at temperatures where steel softens. Change a pin's flute profile and the same weld schedule becomes either a stable process or a defect generator. This is why experienced FSW engineers describe the tool, only half-jokingly, as "where the process lives."
Why tool design is accumulation, not invention. A tool is designed for one combination of alloy, thickness, joint type, and machine. Each new program starts from a known design, then iterates: weld, cross-section, metallography, adjust geometry, weld again. Every iteration produces data — and that data, accumulated across thousands of programs, is what lets an experienced team converge in days instead of months. This is the real barrier to entry in friction stir welding, and it cannot be bought with equipment.
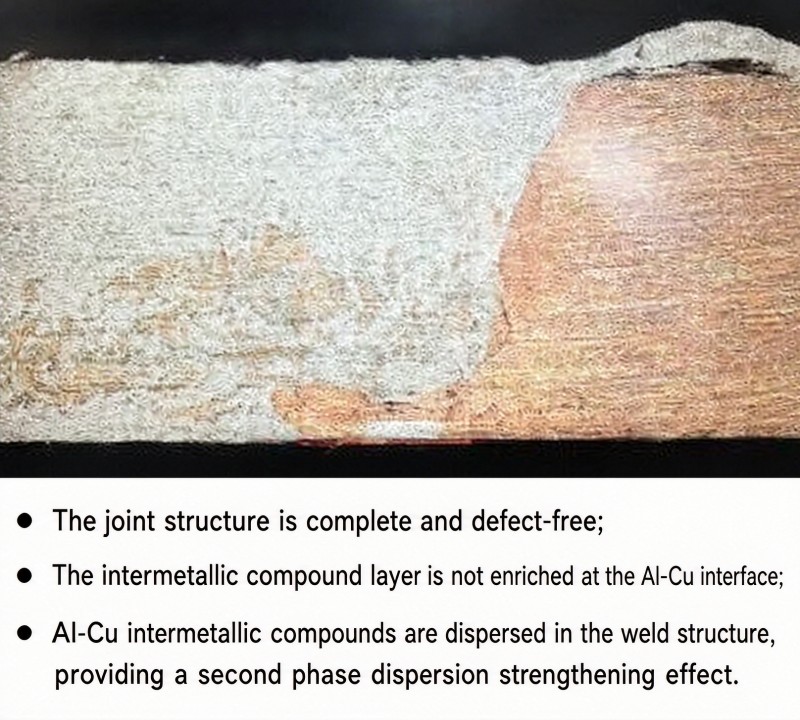
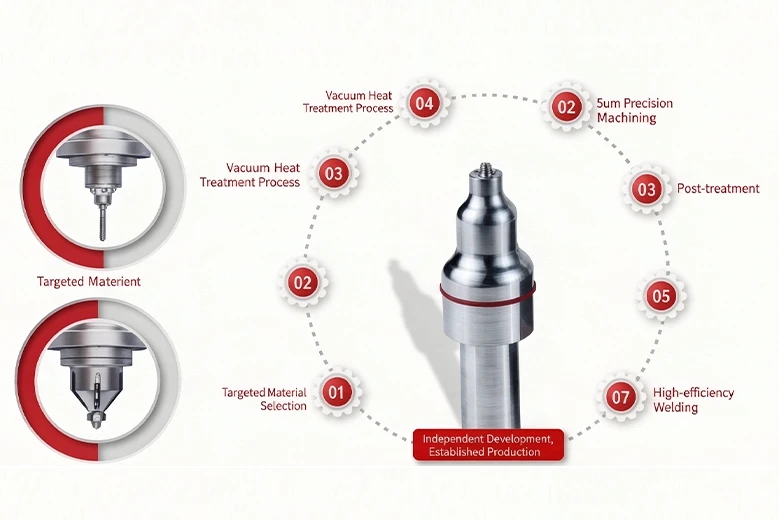
Inside a tool division. Deyanfu runs a dedicated stirring-tool business unit that has developed more than 1,000 tool designs, backed by an accumulated welding-parameter and tooling-process database. In practice that library converts directly into three customer-facing capabilities. Custom design: when a joint involves an unusual alloy pairing, an unequal-thickness stack, or a cast-to-extrusion combination, a tool is developed for that joint rather than forcing the joint to fit a standard tool. Technical service: the same team that designs tools supports customers' welding processes directly, transferring parameters validated on production equipment. And after-sales support: process-critical tooling is backed by 7×24 response — because a worn or broken tool on a running line stops the line.
How a buyer benefits. If you are qualifying FSW suppliers, the tooling question is the highest-signal question available. Ask how many tool designs they have run at production volume — and for your specific joint. Ask to see cross-sections and joint-strength data, not just equipment lists. Ask who designs the tools: an in-house division iterating with its own welding database, or a catalog purchase from a third party. The answers separate a process owner from a process operator.
The wider lesson. In mature manufacturing industries, the deepest moats are rarely the machines — machines can be bought. The moats are the databases, the tooling libraries, and the iteration loops that turn each program's lessons into the next program's starting point. In friction stir welding, that moat is physically small enough to hold in your hand, and metallurgically deep enough to take a decade to cross.
LATEST NEWS
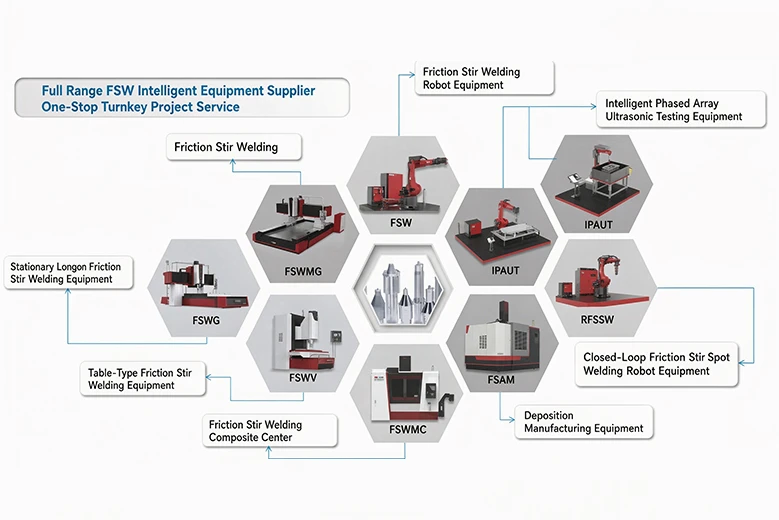
What is friction stir welding (FSW)? How does this solid-state process deliver low-distortion, leak-free aluminum welds for EV battery trays and liquid cold plates? A manufacturer's guide.
Sep.28,2026
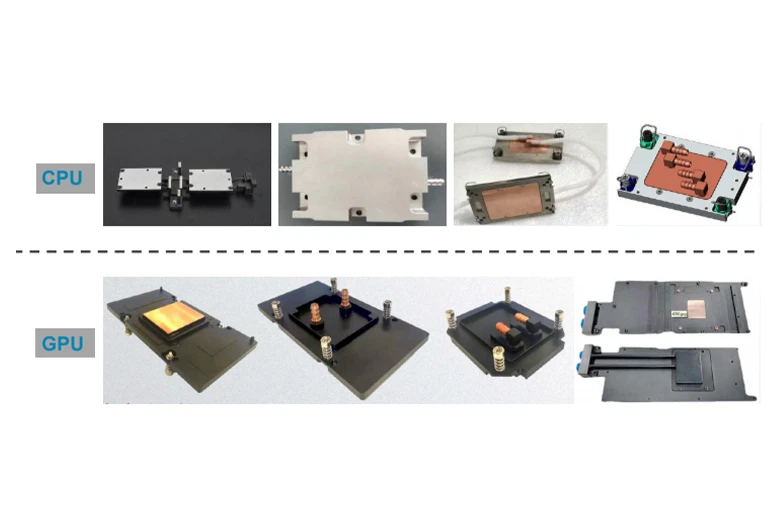
From AI Data Centers to 800V EVs: What It Really Takes to Manufacture Liquid Cold Plates
Liquid cooling is going mainstream in AI servers and EVs. A look inside liquid cold plate manufacturing: flow channel design, FSW sealing, burst and leak testing, and mass production.
Sep.28,2026
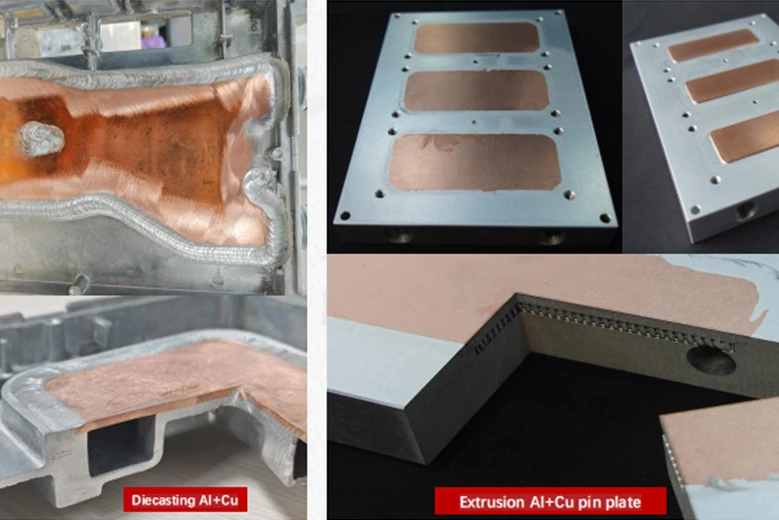
Every hardware generation asks the same question: can we combine two metals in one part — copper for conductivity, aluminum for weight, titanium for strength — without the joint becoming the weakest link?
Sep.28,2026
Refill Friction Stir Spot Welding: A Cleaner Alternative to Resistance Spot Welding and Riveting
Ask a manufacturing engineer how they join two overlapping aluminum sheets, and the answer is usually one of two things: resistance spot welding (RSW) or self-piercing rivets (SPR). Both work. Both also carry costs that product designers have learned to live with — until a solid-state alternative called refill friction stir spot welding (RFSSW) matured into mass production.
Sep.29,2026
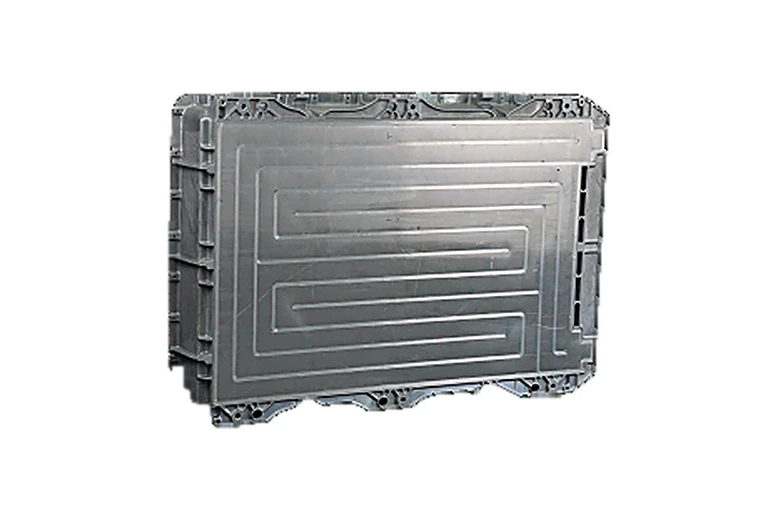
Case Study: Friction Stir Welding ADC12 Cast Aluminum to 6061 Extrusions in a Bus Battery Tray
Modern battery trays are a metallurgy puzzle wearing a structural role. The tray must be light, crash-stiff, leak-manageable, and cheap — so designers mix material forms: die-cast nodes and bosses for complex geometry, extruded profiles for rails and frame members, and rolled plate for covers. Each form is easy to make alone. Joining them is the problem, and a recent bus battery tray program shows how one manufacturer solved it.
Sep.29,2026
How to Specify and Accept Liquid Cold Plates: Burst, Pressure Drop, Leak and Thermal Tests Explained
Most cold plate quality disputes trace back to the same root cause: the buyer and supplier never agreed on what "good" means, in test terms. A liquid cold plate can pass a visual check and still fail in the field — clogged channels, creep leakage at a pulse-loaded seam, or a heat-absorbing surface that is out of flatness. Here is the test matrix that serious manufacturers and serious buyers use to align expectations, item by item.
Sep.29,2026
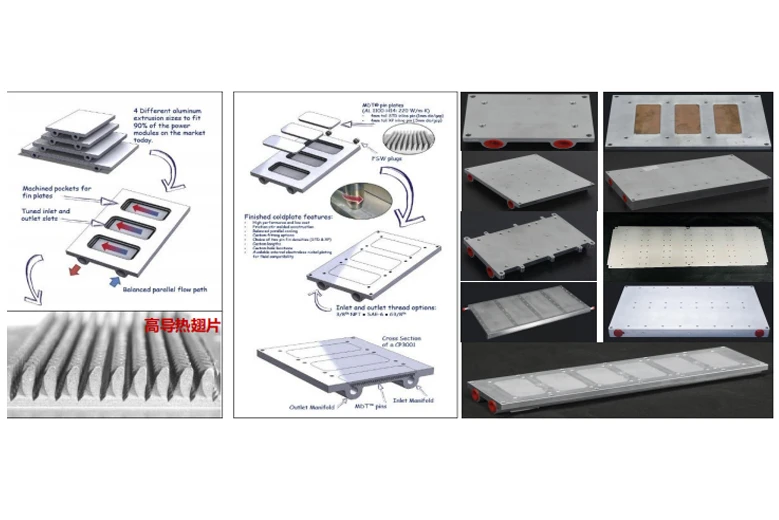
For most of computing history, "thermal management" meant fans. Air cooling defined the shape of servers, the layout of data centers, and the limits of every processor design. That era is ending. AI rack densities that once would have been measured in kilowatts are now quoted in multiples of 100 kW, and no quantity of fans can move that heat out of a rack economically. The industry's answer is direct-to-chip liquid cooling — and its rise is quietly rebuilding a supply chain around a component most data center buyers had never sourced before: the liquid cold plate.
Sep.29,2026
The Overlooked Heart of Friction Stir Welding: Inside a 1,000+ Tool Design Library
Friction stir welding has a paradox at its center. The physics — a rotating tool that plasticizes and forges metal without melting it — is elegant, widely published, and more than three decades old. The equipment is now sold by several vendors worldwide. Yet weld outcomes between two suppliers running identical machines on identical alloys can differ by a wide margin. The variable that explains most of the gap is the smallest, least glamorous part of the system: the stirring tool itself.
Sep.29,2026
"Need a Custom Cold Plate for Your Application?
Request a Free Thermal Design Review"
We provide high-strength, well-sealed core components for new energy vehicles that meet global automotive standards. Schedule a rapid technical consultation now.
Build a highly cohesive team of thermal management, special welding and precision manufacturing
QUICK LINK
QUICK LINK
LET’S CONNECT
LET’S CONNECT
+86 177 1265 6888 (WhatsApp)
+86 137 7167 8566 (WhatsApp)
Peter Fu peter@dyf-sz.cn
Eva Zhou deyanfumachinery@gmail.com
Building 3, No. 28 Xinchang Road, Suzhou Industrial Park, Suzhou City, Jiangsu Province